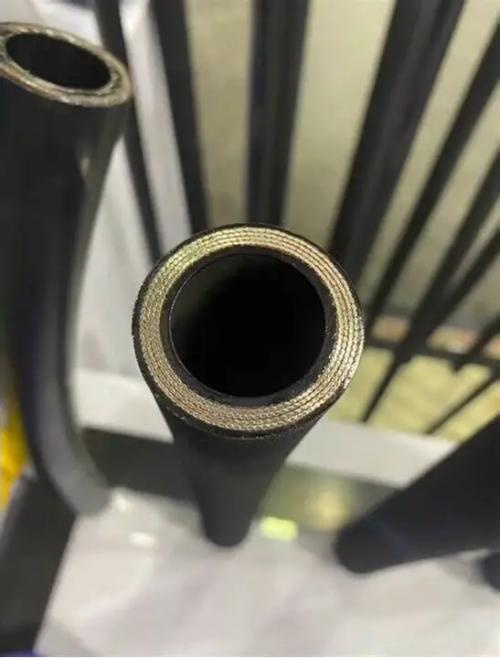
Large Diameter High Pressure Hydraulic Hose
Steel wire braided hose assemblies are used in hydraulic systems, construction machinery, mining equipment, marine piping, and industrial fluid transportation for the flexible transmission of media such as pressurized oil, water-based hydraulic fluids, compressed air, and water. Their working pressure range is wide, ranging from several MPa to tens of MPa, depending on the number of braided layers and the pipe diameter.
II. Structural Design and Material Composition
Inner Layer (Inner Rubber Layer): Material selection depends on the type of media being transported. For hydraulic oil and mineral oil-based media, nitrile rubber (NBR) is typically used for the inner layer. The polar nitrile groups in its molecular structure give the material excellent resistance to mineral and synthetic oils. For water, water-glycol, and aqueous media, ethylene propylene diene monomer (EPDM) rubber or styrene-butadiene rubber (SBR) can be used. For special media such as phosphate ester hydraulic oil, EPDM or butyl rubber must be selected. The inner layer thickness is typically between 1.5mm and 3.0mm, depending on the hose's inner diameter and pressure rating.
Reinforcing Layer: Employs a high-strength steel wire braided structure. The number of braided layers is determined by the pressure rating, commonly one, two, or four layers. The steel wire is made of high-carbon steel with a tensile strength of not less than 1800MPa, and is copper- or zinc-plated to enhance adhesion to the rubber. The braiding angle is controlled around 54°44' to balance radial pressure resistance and axial flexibility. In the multi-layer braided structure, an intermediate rubber layer is provided between each layer to ensure strong interlayer adhesion. The number of steel wires and braiding density in each layer are precisely calculated based on the pressure rating and inner diameter specifications.
Outer Layer (Outer Rubber Layer): Primarily made of wear-resistant and weather-resistant synthetic rubber, typically a blend of chloroprene rubber (CR) or nitrile rubber and polyvinyl chloride. The outer layer must possess oil resistance, wear resistance, weather aging resistance, and ozone resistance to withstand oil, ultraviolet radiation, ozone, and mechanical friction in industrial environments. Some products add flame retardants to the outer layer to meet flame retardant requirements in mining and marine applications.
Crimped Fittings: The core connecting component of the assembly, permanently connecting the metal fitting to the pipe body through a crimping process. The crimping process uses external force to plastically deform the metal outer sleeve, tightly pressing the hose body onto the fitting core, creating a dual effect of mechanical locking and sealing. The fitting material is typically carbon steel or stainless steel, with a galvanized or passivated surface to improve corrosion resistance. Fitting types include metric threads, imperial threads, NPT threads, flanges, and quick-connect fittings, adaptable to different piping system interface specifications.
III. Core Performance Parameters
Working Pressure: Depending on the number of braids and inner diameter, the working pressure ranges from several MPa to tens of MPa. More braids result in a higher pressure rating; for the same number of braids, a larger inner diameter results in a relatively lower pressure rating.
Burst Pressure: Not less than 3 to 4 times the working pressure, providing ample safety margin.
Pulse Life: Under pressure cycling conditions, the hose assembly must have sufficient fatigue life to meet the requirements of frequent pressure fluctuations in hydraulic systems.
Temperature Range: Standard products operate from -40℃ to +100℃, with some products extendable to +120℃.
Inner Diameter Specifications: Common inner diameters range from 5mm to 51mm, including 1/4 inch, 5/16 inch, 3/8 inch, 1/2 inch, 5/8 inch, 3/4 inch, 1 inch, 1-1/4 inch, 1-1/2 inch, and 2 inch sizes.
Minimum Bending Radius: Related to the inner diameter and braided layer structure, the minimum bending radius of a steel wire braided hose assembly is typically between 5 and 8 times the hose diameter.
IV. Assembly Manufacturing and Quality Control
Hose Body Manufacturing: The hose body undergoes processes such as inner layer extrusion, steel wire braiding, outer layer extrusion, and vulcanization. Vulcanization causes a cross-linking reaction in the rubber, bonding the layers into a unified structure.
Connector Crimping: Crimping is a critical process in assembly manufacturing. Crimping pressure, crimping amount, and crimping length are the core parameters determining crimping quality. Insufficient crimping pressure will result in insufficient connection strength between the connector and the hose body; excessive crimping pressure will cause over-compression of the hose reinforcement layer, reducing the pressure-bearing capacity of that area. The crimping amount needs to be accurately calculated based on the hose inner diameter, reinforcement layer structure, and connector specifications.
Sealing Performance Test: After crimping, a sealing performance test is required at the connection area between the connector and the hose body. This is typically performed at 1.5 times the working pressure for a certain period of time, observing for any leaks.
Tensile strength verification: The connection strength between the joint and the pipe body must meet the requirement of not axial slippage or detachment under the design pressure.
Identification and traceability: Assemblies are typically marked with specifications, pressure rating, temperature range, and manufacturing batch number on the pipe surface for easy identification and quality traceability during use.
